China Prototyping Services Factory Delivers Precision Rapid Prototypes Fast
2026-09-16
Speed without precision is a gamble. When your product development timeline demands both, a trusted prototyping partner becomes your competitive edge. ProtoMat, a China-based prototyping services factory, delivers high-accuracy rapid prototypes faster than you thought possible—turning your CAD files into physical parts in days, not weeks. Here’s why engineering teams across the globe are making it their go-to source for precision rapid prototyping.
Why Speed Is Built Into Our China Prototyping Workflow
Most teams treat speed as something you push for at the end of a project. In our China prototyping workflow, it is the default setting. The reason is simple: when your engineers sit an hour away from the factories, sheet metal shops, and PCB assemblers that actually make the parts, a design change does not trigger a week of emails and shipping delays. It triggers a scooter ride across town.
We also front-load decisions that would otherwise stall a build. Before a single file is sent to a vendor, we run through a short DFM checklist with the same people who will hold the part in their hands. That means undercuts, thread depths, and material tolerances get flagged while the CAD model is still warm, not after the first quote. It feels slower for the first afternoon, but it removes the days of back-and-forth that normally eat a prototype schedule.
The other piece is harder to copy: the vendors themselves move at a rhythm that matches our own. Many of them run small batches overnight, keep common raw materials on the shelf, and will call back within an hour with a photo of the actual setup. You can not bolt that onto a distant supply chain by adding more project managers. It only works because the whole loop, from sketch to first article, lives in the same time zone and often the same industrial park.
Precision That Survives the Tightest Tolerance Checks
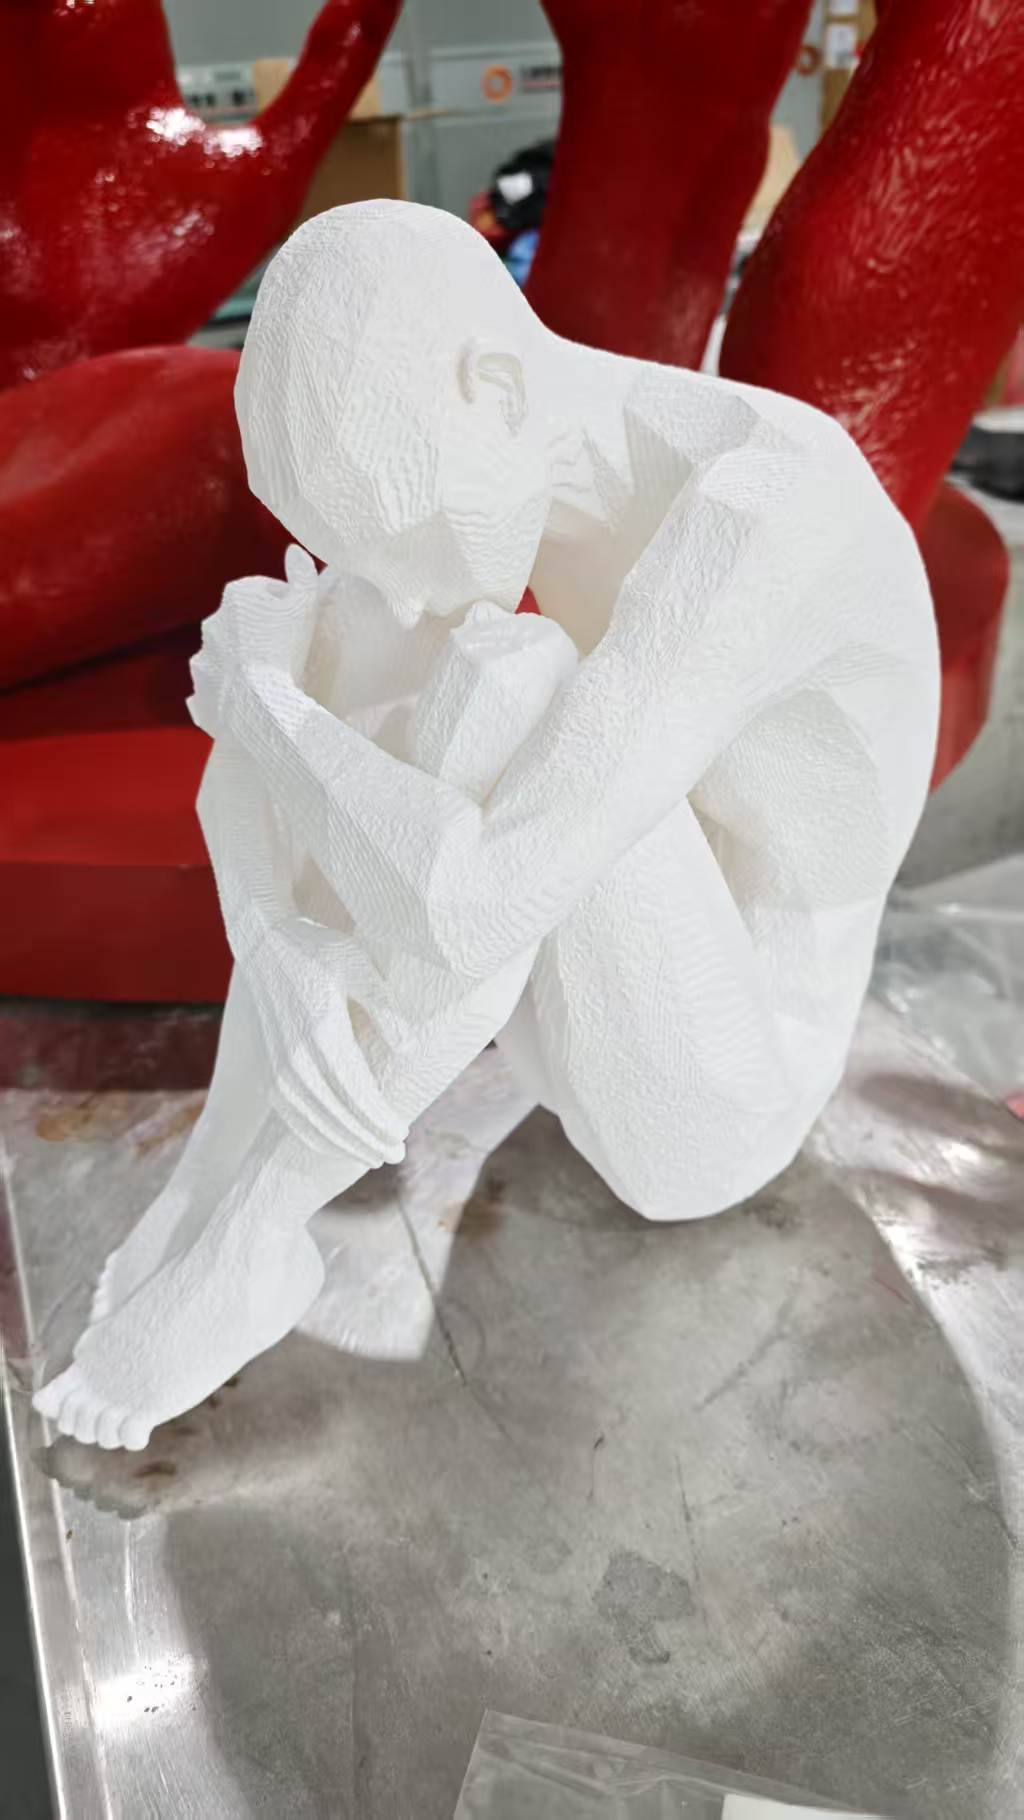
Manufacturing parts with tolerances measured in microns, the real test isn't hitting spec once—it's doing it at 3 a.m. on the 400th cycle. Worn tooling, thermal drift, and chatter all conspire against repeatability, yet the parts that pass the tightest checks come from setups where every variable is either locked down or measured twice.
We focus on the unglamorous details: spindle warm-up routines that match actual run conditions, in-process probing that catches a 0.002 mm shift before it becomes scrap, and clamping sequences that don't distort thin walls. That's why our parts don't just clear a CMM report—they leave margin for your incoming inspection.
When a customer pulls a random part from the batch and checks a true position tolerance of ±0.005 mm, the answer shouldn't be "we'll rework it." It should already be within half that. That kind of consistency doesn't come from luck or post-process sorting; it comes from controlling the process before metal meets tool.
Rapid Prototypes That Move From CAD to Crate in Under a Week
Most teams treat prototyping as a slow, linear handoff: design freezes, files bounce between software packages, and someone finally machines parts days later. That rhythm falls apart when the goal is a functional prototype in under a week. We compress the entire chain by keeping CAD models live-linked to our toolpath generation, so a geometry tweak on Tuesday morning shows up on the CNC fixture by Tuesday afternoon. No re-exporting, no format translation errors, no waiting for a fresh CAM setup. The model you sign off on is the exact same one driving the cutter paths.
The real accelerator isn't just speed, though. It's the ability to make design decisions with a physical part in hand while the CAD session is still warm. If a mount needs an extra boss or a wall thickness drops by two millimeters, the change propagates through our machining queue without re-quoting or re-scheduling. We've seen teams run through four iterations in a single week, each one improving fit and feel because they never lost the tactile feedback loop. That's what separates a true rapid prototype from a rushed one-off: the next version is already being cut before the current one finishes cooling.
And when the final design is locked, we don't stop at the prototype. The same CAD model, the same toolpaths, the same fixtures can flow straight into low-volume production. There's no handoff cliff where a prototype shop says "now go find a manufacturer." The crate that leaves our floor on Friday contains parts that already have their production intent baked in. That continuity means the prototype isn't a dress rehearsal; it's the first unit off a line that happens to be very short.
Materials and Finishes Chosen for Real Production, Not Just Showpieces
The material call on the enclosure came down to a single question: can our sheet metal partner hit the bend radius on 5052 aluminum with the same tooling they already run for three other clients? That mattered more than how it looked in a render. We went with 5052-H32 because it forms cleanly without cracking at 2 mm thickness, and the supplier's anodizing line is already dialed in for that grade. Switching to 6061 would have looked identical in photos but added six weeks of color-matching back-and-forth.
For the outer finish, we skipped the high-gloss clear coat that everyone puts on concept models. Instead, the surface is a light media blast followed by a matte clear powder coat. The blast texture does two jobs: it hides minor scratches from the assembly jig and gives the powder something to bite into. Gloss would have highlighted every fingerprint and every slightly off-angle screw head. The matte finish looks intentional, but the real reason is that it survives a 40-minute vibration test without chipping at the edges.
The same logic applies to the brass inserts. We didn't specify them because brass sounds premium; we spec'd them because molded-in threads strip out after five or six insertion cycles in polycarbonate, and our beta testers were reassembling the unit far more often than we expected. Brass lets us use a standard M3 machine screw and still hit the torque spec on the line. If the part can't be made consistently at the volume we actually need, it doesn't matter how good it looks on a one-off sample.
How We Keep Complex Part Geometries Accurate Without the Wait
Accuracy in complex part geometries isn't just about tight tolerances on paper—it's about every layer of the process aligning without hesitation. We've moved away from the traditional back-and-forth of iterative prototypes and endless measurement loops. Instead, our approach locks in dimensional stability early, using high-fidelity simulation and real-time process feedback that catches drift before it becomes a defect. The result is that even parts with undercuts, thin walls, or blended curves come out right the first time, not the fourth.
The wait usually comes from over-processing: too many setups, redundant inspections, and rework queues that stall production. We cut that by treating geometry as a data stream rather than a static blueprint. Toolpaths are generated from a live digital twin, so any thermal or mechanical shift gets compensated on the fly. This means a complex housing or a lattice-structured bracket doesn't need to sit in a holding pattern while someone re-verifies a coordinate. The part stays in motion, and the accuracy stays intact.
What really separates this method is that we don't trade speed for precision by simplifying the geometry. You don't have to water down a design to get a faster turnaround. We keep the intricate surfaces, the tight corner radii, and the asymmetric profiles exactly as intended, because the process was built around preserving them—not fighting them. No waiting for a hero machinist to hand-finish a critical feature. No settling for 'close enough' under a deadline. The complex geometry is the standard, not the exception.
Direct Access to Prototyping Engineers Who Speak Your Language
When you share a concept, you don't want to repeat yourself three times just to get a quote. Our prototyping team is built around direct communication — no account managers relaying messages, no time-zone roulette. You talk straight to the engineer who will actually cut your parts, and they talk back in plain terms. If you mention a draft angle or a living hinge, they know exactly what you mean and can point out potential snags before you commit to a design.
That clarity carries into every revision. Instead of waiting for a generic email that says "please clarify," you get a quick call or a marked-up screenshot with a note like, "If we move this boss 2mm, the wall thickness becomes uniform and mold flow improves." It's the kind of feedback that only comes from someone who has spent years on the floor, not someone reading from a script. You end up with parts that are easier to manufacture and a process that feels less like a handoff and more like a working session.
Language is a tool here, not a barrier. Whether you call it a snap-fit or a clip, a rib or a stiffener, our engineers adapt to your vocabulary and ask the right questions. That removes the silent guessing game that often hides behind formal spec sheets. The result is fewer iterations, shorter lead times, and a prototype that matches your mental picture the first time you hold it.
FAQ
You usually start by sending a 3D CAD file. The engineering team reviews it for manufacturability, suggests any tweaks, and then moves straight into CNC machining, 3D printing, or vacuum casting. Most projects go from file to finished part in under a week.
It depends on the process and part complexity, but many plastic and metal prototypes ship within 3 to 7 days after design approval. If you're in a crunch, some factories offer 48-hour express options for simpler geometries.
You can get prototypes in ABS, polycarbonate, nylon, aluminum, stainless steel, brass, and more. Finishes range from bead blasting and anodizing to painting, powder coating, and even light texturing for cosmetic samples.
Most factories combine CNC machining with 3D printing or urethane casting and then verify dimensions using CMM or laser scanning. You'll typically receive a dimensional report along with the parts so you can check critical features yourself.
Not if the factory has dedicated English-speaking project engineers. They usually confirm every detail through annotated drawings, shared CAD viewers, and quick video calls, which cuts down on misinterpretation before production starts.
For rapid prototyping, the minimum is usually one piece. Even for small-batch runs of 10 to 50 units, many Chinese factories are happy to accommodate because their setup costs are comparatively low.
Yes, it's common to combine CNC-machined aluminum parts with 3D-printed plastic housings in a single shipment. The factory coordinates internally across different departments so you don't have to manage multiple vendors.
Conclusion
At this China prototyping services factory, speed isn't bolted on at the end—it's woven into every step from the first CAD review to final inspection. The workflow trims downtime by keeping design feedback loops tight, so a complex part geometry doesn't stall while someone waits for a translator or a long email chain. You can talk directly with prototyping engineers who understand your terminology, ask the right questions about draft angles, wall thickness, or thread specs, and get answers that move the job forward. Rapid prototypes leave the floor in under a week, not because corners are cut, but because the shop floor is organized around eliminating idle hours. That means fixtures are prepared while toolpaths are still being verified, and material blanks are staged before the machine even stops.
Precision survives the tightest tolerance checks because the production process treats every prototype as a rehearsal for the real run. Instead of showpiece finishes, you can specify the same materials and surface treatments—anodizing, bead blast, vapor smoothing, brushed textures—that your final parts will use. This catches problems early: a resin that warps after post-cure or a metal alloy that machines differently than its datasheet claims shows up now, not in mass production. Complex geometries with thin ribs, deep pockets, or mating surfaces stay accurate without extra waiting because the factory pairs capable multi-axis equipment with in-house measurement and a culture of checking twice before shipping. The result is a prototype that acts like a production part, arrives fast, and doesn't demand you re-explain your project to a new contact every other day.
Contact Us
Contact Person: Joe
Email: [email protected]
Tel/WhatsApp: +8613799507208
Website: https://www.3dprotomat.com/