Open Type Fiber Laser Cutting Machine Factory Practical Selection Guide
2026-10-14
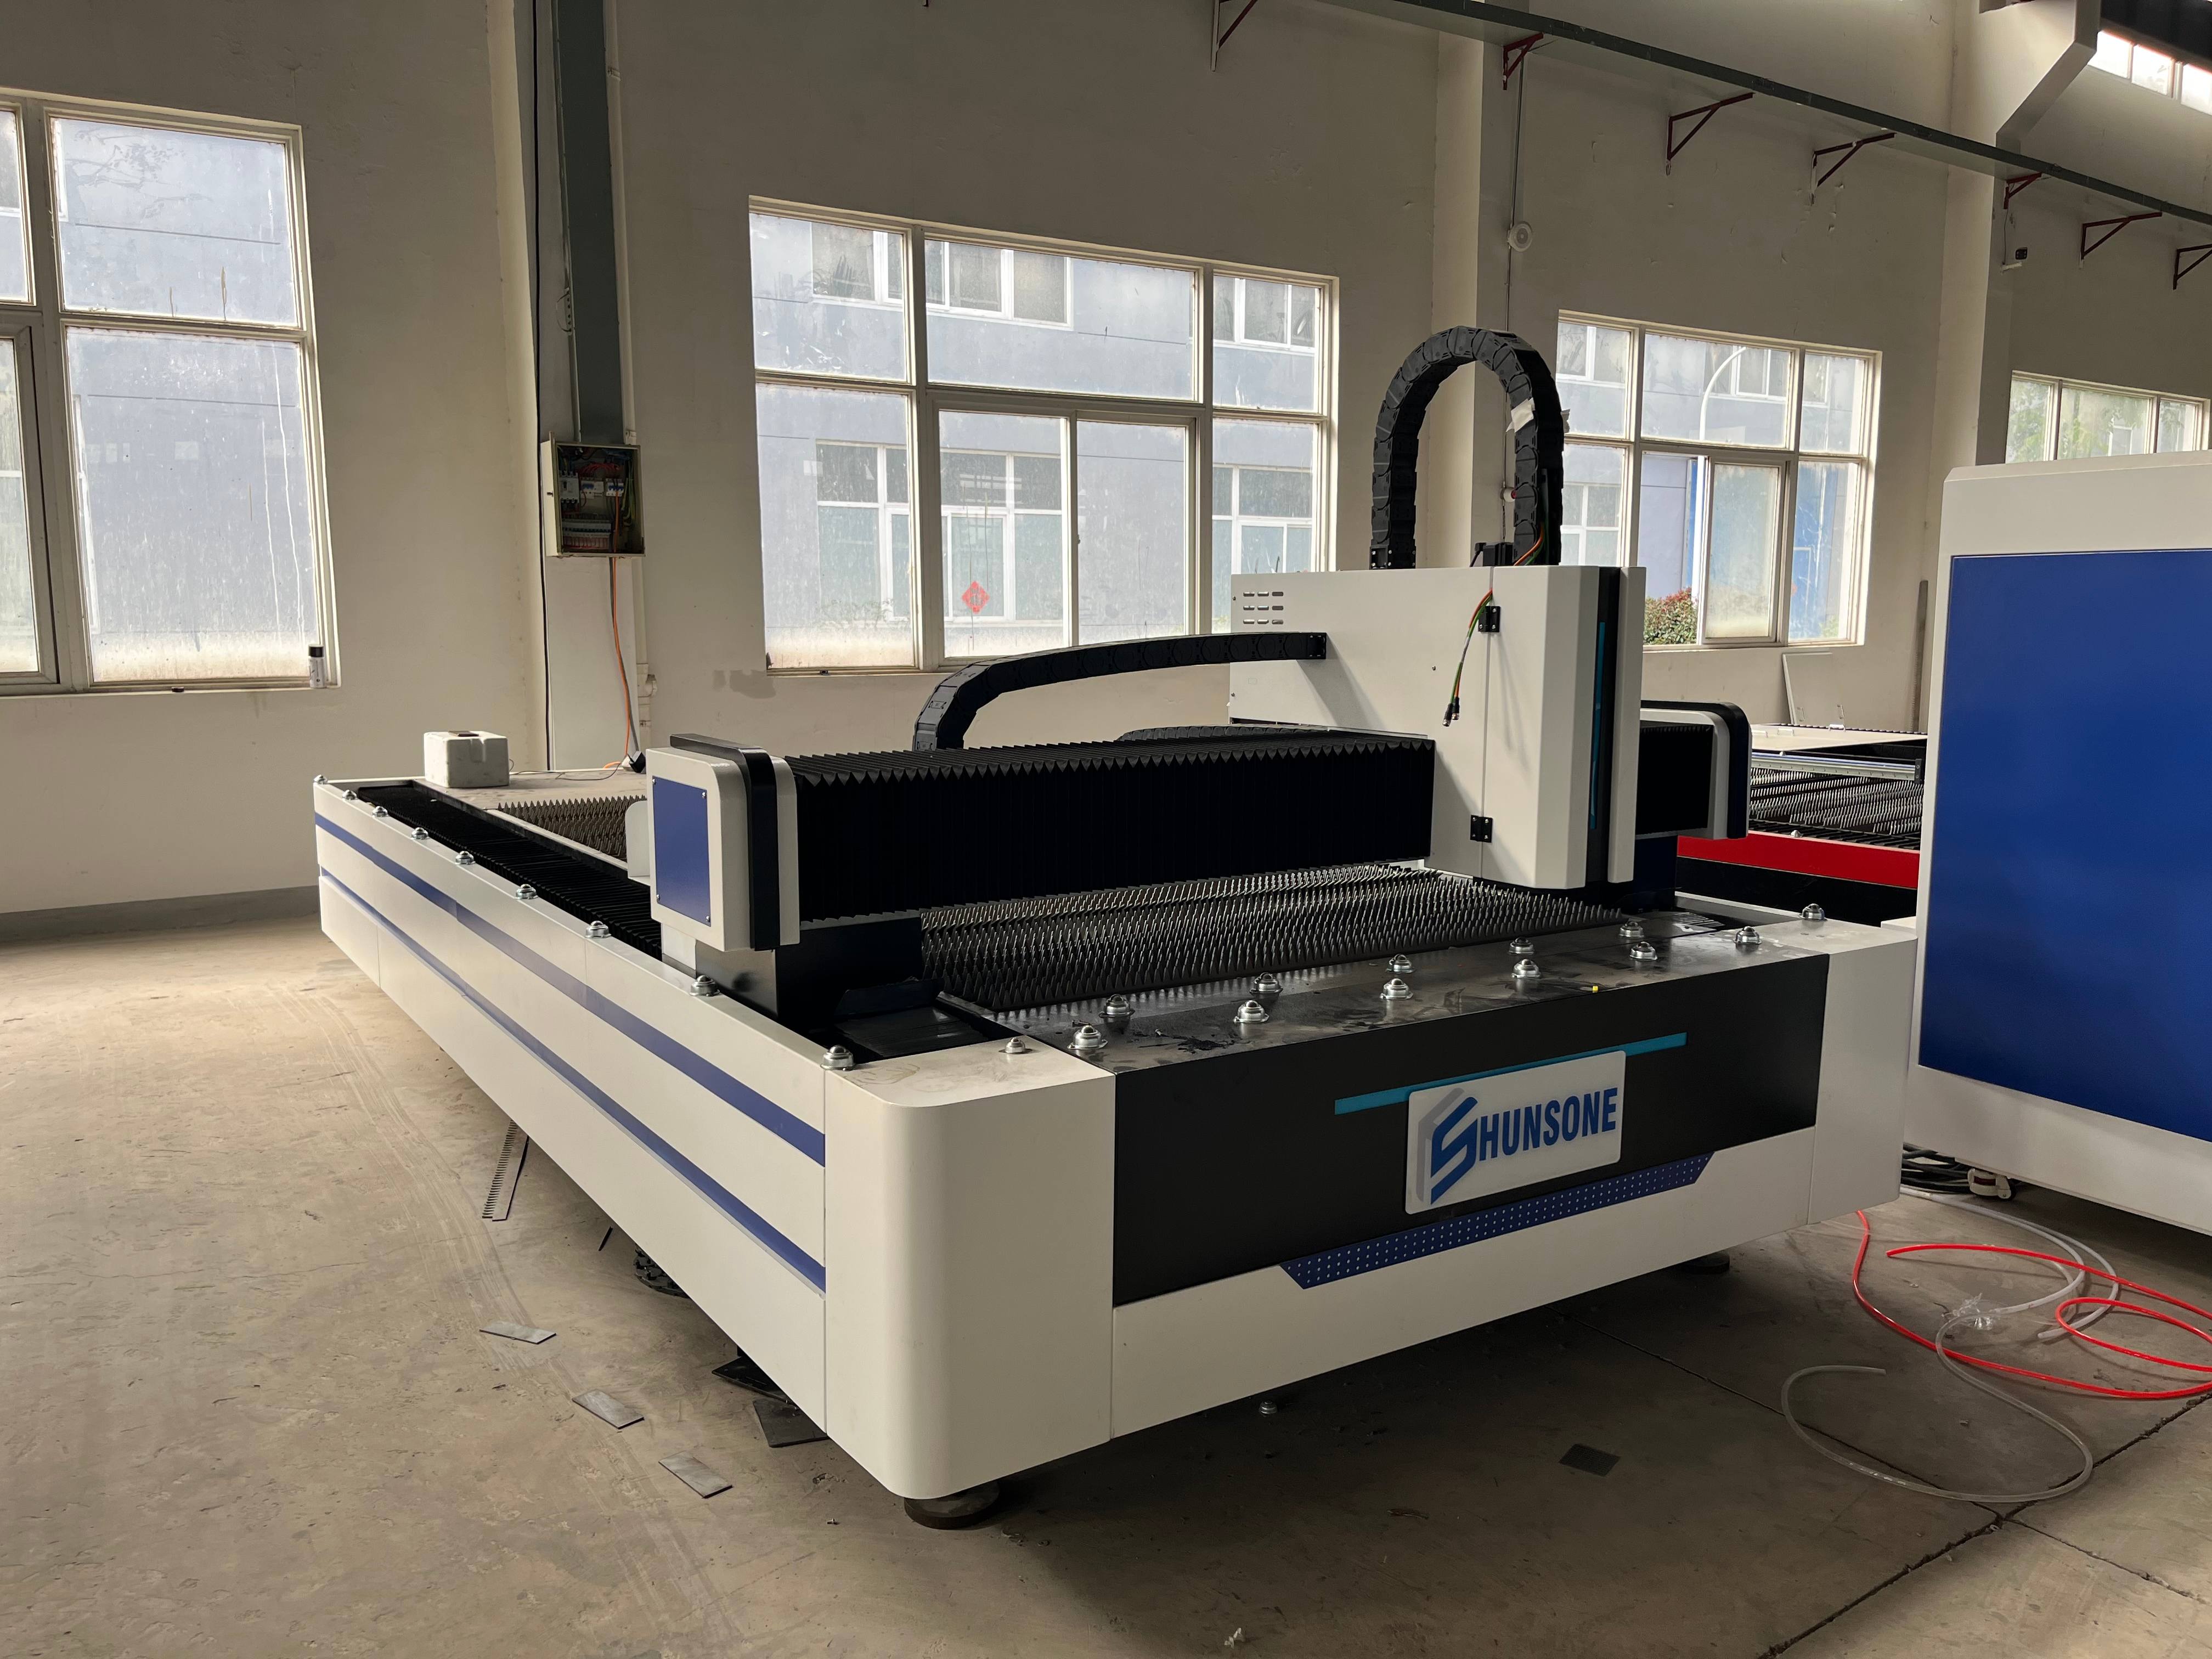
If you’re sourcing an open type fiber laser cutting machine for your factory, you already know the advertised specs aren’t the whole story. Real selection involves asking questions most guides skip: how the frame handles thermal stress, whether the protective covers actually survive daily use, and how easy it is to get service when something goes wrong. This guide cuts through that noise—with a close look at what separates dependable suppliers like HUNSONE from the rest.
What a Factory Floor Reveals Before Anyone Says a Word
The first thing that hits you isn't a sound but a texture—how the light falls on worn concrete, where the yellow safety lines have faded unevenly, and whether the tool shadows on the pegboard match the tools currently in use. A floor that's swept but not polished tells you the crew values function over show. A stray pallet angled against a support beam, left there for days, hints at a workflow bottleneck nobody has bothered to resolve. These details speak in a dialect older than any shift briefing: the physical space itself is a ledger of habits.
Watch two workers pass each other near the conveyor. Do they acknowledge each other with a nod, a half-smile, or nothing at all? The distance they keep, the speed of their stride, even the way they hand off a scanner or a wrench—these micro-gestures map the invisible power lines of the team. In some plants, a supervisor's presence changes the rhythm of the line without a single order being given. In others, the line hums on as if no one is watching, because no one is. That tells you more about trust than any employee survey ever could.
Then there's the maintenance calendar pinned near the entrance, with dates crossed out in different pens, some faded, some fresh. If the last entry is three weeks old but the dust on the machine covers is thicker than that, you've found the gap between what's documented and what's done. Safety signage with updated revision numbers next to an unlabeled chemical drum reveals a management that audits but doesn't act. A factory floor doesn't just produce goods—it produces evidence, every minute, about who actually runs the place and what they're willing to let slide.
Matching Cutting Bed and Power to Work Orders, Not Wish Lists
A cutting table only earns its footprint when it's sized to the actual spread length, ply height, and knife travel your confirmed orders demand. Too often, shops buy extra bed length or vacuum zones based on what marketing sheets hint they might cut someday, then realize the monthly power bill is feeding dead air. Start with the longest marker in your current queue, add buffer for splices and end losses, and let that dictate the bed you actually pay to run.
The same logic applies to compressor sizing and vacuum hold-down. A system that can pull 25 horsepower of suction sounds impressive, but if your thickest stack is denim at 40 plies, you're likely overspending on peak capacity that never gets used. Work backward from your densest, most difficult lay — the one that actually tests hold-down — and size the pump to that, not to a fantasy of cutting upholstery foam next quarter.
Put a hard rule in place: no new cutting equipment gets approved without a written list of the last thirty work orders it would have run. If the list shows the same narrow range of materials and spreads over and over, buy for that range. Wish lists create idle capacity, and idle capacity on a cutting bed shows up as higher energy draw, more frequent maintenance, and operators waiting on a machine that was built for a job you never signed.
Why Two Open-Type Machines with the Same Specs Cut Differently
Same specs on paper rarely translate to identical cuts because specs list broad ranges, not the actual assemblies sitting in the shop. On an open-type machine, minor differences in gib tightness, leadscrew backlash, or the way the table was leveled during installation show up directly at the cut line. One machine may have settled slightly out of tram after moving, while the other is still square, so identical feed and speed settings produce noticeably different kerf width, surface finish, or drift.
Cutting behavior also shifts with wear that specs never capture. If one machine has seen more abrasive materials, its guides and drive belt may have developed small amounts of play, turning what should be a straight cut into a slight wave. Tool condition matters too; a blade or cutter that looks identical can have micro-chips or uneven honing from a previous job. These invisible differences change how material is removed, so two machines with the same horsepower and RPM can sound and cut completely different.
On open-type machines, the surrounding environment plays a bigger role than people expect. One unit near a bay door may expand and contract with drafts or sunlight, shifting alignment through the day. Another with slightly more coolant residue on the ways may have stick-slip that changes feed feel. Operator habits add another layer: the same blade tension set by hand will vary between two people, and that alone can make one machine cut straight while the other wanders.
Hidden Running Costs That Surface After the First Service Call
You sign the contract, pay the initial invoice, and assume the worst is behind you. Then the first maintenance visit happens, and suddenly the bill includes line items you never saw coming. Consumables that were supposedly covered show up as extra charges. A minor adjustment turns into a recommended replacement part with a markup that makes your eyes water. The real shock isn't the price of the machine itself, it's the quiet drip of fees that only appears once a technician walks through your door.
Many businesses budget for the obvious expenses, but few plan for the so-called 'incidentals' that pile up after that first service call. Software licenses need renewing, calibration requires a specialized tool you don't own, and labor minimums mean even a five minute fix costs a full hour. These aren't hidden in fine print as much as they're never mentioned until you're standing next to an open panel. The result is a monthly operating cost that's noticeably higher than the quoted estimate, and nobody can tell you why until you start comparing invoices.
To avoid the surprise, ask your provider for a complete list of what a standard service visit includes and what gets billed separately. Request examples of past invoices from customers with similar equipment. If a salesperson hesitates or says 'it depends,' push for real numbers. The companies that are upfront about these costs tend to be the ones you can trust long term, while the ones that dodge the question are often the reason your budget spreadsheet keeps needing new columns.
Checking Component Origins Without Relying on Sales Claims
A supplier's pitch can sound convincing, yet the actual origin of a component often shows up in details that salespeople never mention. Rather than taking a data sheet or verbal assurance at face value, start with the physical part itself. Look closely at markings, logo consistency, date codes, and the quality of lead finishes or plating. Counterfeit or relabeled parts frequently have subtle irregularities—blurred text, mismatched fonts, or slightly off dimensions—that a genuine item from the original manufacturer would not show.
Beyond the surface, request documentation that ties the component to a specific production batch. A certificate of conformance might be easy to forge, so cross-check the lot number and date code against the manufacturer's own records where possible. Many established manufacturers offer online verification tools or direct inquiry channels. If the supplier hesitates to share batch-level detail or gives inconsistent numbers, that alone is a warning sign worth investigating before the parts reach your production line.
For high-risk or high-value components, independent testing adds another layer of certainty. Simple electrical tests can catch re-marked lower-grade parts, while X-ray or decapsulation analysis can reveal internal die markings and construction. Keep a log of what you find—measured dimensions, test results, and supplier responses—so you can spot patterns over time. This practical approach turns origin checking from a matter of trust into a repeatable process based on evidence.
Turning a Factory Visit into a Real Stress Test
Most factory tours stick to the polished aisle, the scripted demo, the safety goggles that never get scuffed. A real stress test starts before you pass the gate: watch how the shift handover is handled, whether the maintenance log has gaps, and whether the person guiding you can answer "what broke last week" without checking a script. These quiet signals reveal far more than any spec sheet.
Push past the planned route. Ask to see the quarantine area for rejected parts, the rework bench, the overflow storage. If the tour guide hesitates or redirects, that’s a data point in itself. A factory that treats a visitor like an auditor—openly pointing out chronic bottlenecks or a line that ran hot last month—is signalling confidence, not weakness. The ones that hide those corners are usually hiding something else.
Finally, invert the usual question. Don’t ask “can you hit this volume?” Ask “what conditions make you miss it?” Every plant has a failure mode: a supplier that slips, a fixture that drifts, a shift that runs short-handed. If the operations lead can describe their failure modes without flinching, you’ve moved from a tour to a test.
FAQ
Look at how the gantry and bed are machined, not just the spec sheet. Ask to see the stress-relief process for welded frames; if they can't show it, walk away. A stable open frame matters more than extra laser watts for repeatable cuts.
It depends on the frame mass and drive system, not whether there's a full enclosure. A well-built open machine with a heavy bed and dual-drive gantry can handle 20 mm mild steel without losing accuracy, but the torch height control and cutting head rigidity become critical beyond that.
Match the power to your thickest regular job, not the occasional job. If 80% of your work is under 6 mm, a 3 kW source with good assist gas dynamics will cut faster and cleaner than an underused 6 kW that sits at 40% duty. Ask the factory for real cutting time samples, not just published max speeds.
Yes, because an open frame lets fumes and heat drift upward into the optics and linear rails. A dual-circuit chiller with precise temperature control isn't an upsell—it's what keeps the resonator alive during long shifts. And don't skip a fume extraction arm; your lens cleaning schedule will thank you.
Request a live nesting demo with your own DXF files. The difference between a generic controller and a proper fiber cutting software is in lead-ins, corner power ramping, and pierce delay handling. If the tech can't explain how to tweak those, you'll fight the machine every day.
Ask for the service engineer's phone number before paying, and call it. A factory that gives you a direct line to someone who knows the PLC and servo tuning is worth more than a longer warranty on paper. Also check if they stock spare lenses, nozzles, and ceramic rings locally—not just ship them from overseas.
Usually yes, but not because of the logo. Branded heads have better internal optics coating and more consistent focus calibration, which means fewer adjustments when switching from nitrogen to oxygen cutting. The same goes for servos—generic drives may work, but their tuning parameters are often copy-pasted and cause oscillation at high traverse speeds.
They compare only the tube wattage and table size, ignoring the frame's torsional stiffness and the quality of the helical rack. Two machines with the same 4 kW IPG source can cut very differently if one uses a lighter gantry and cheaper rails. Ask for a deflection test report under load, not just CAD renderings.
Conclusion
Walking onto a factory floor tells you more than any brochure. Before a single word is exchanged, you notice whether cables are routed cleanly, whether the gantry moves without hesitation, and whether operators look rushed or confident. That first impression often predicts how the machine will behave after install. Instead of chasing the largest cutting bed or the highest wattage, match the table size and laser power to the parts you actually cut week after week. A 6kW source on a 4x2m bed might sound impressive but becomes a costly ornament if your work orders rarely exceed 3mm mild steel.
Two open-type machines with identical spec sheets can cut like night and day. The difference usually hides in frame alignment, lens quality, and how carefully the linear rails were mounted. Ask to see a real cutting test on your own material, not a pre-selected sample. Watch the assist gas consumption and check filter prices before you buy, because running costs tend to surface only after the first service call. Pop open a panel and look for the brand names on motors, drives, and the laser source—don't rely on a salesperson's word. Finally, treat your factory visit as a stress test: run the machine at full acceleration for an hour, switch between thick and thin sheets, and see if the cutting head stays stable. That hour will reveal more than any datasheet ever could.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/