Top Open Type Fiber Laser Cutting Machines: The Ultimate Guide to Precision and Performance
2026-10-09
When it comes to cutting metal with precision that rivals a surgeon’s scalpel, open type fiber laser cutting machines are rewriting the rules of modern fabrication. But not all machines are created equal—some promise speed, others deliver finesse, and a rare few manage both without breaking a sweat. In this guide, we cut through the noise to explore what truly separates a workhorse from a showpiece. From beam quality to thermal stability, we’ll unpack the engineering secrets behind top-tier performance. And if you’re ready to see how HUNSONE pushes the boundaries of open type design, stick around—the details ahead might just change how you think about laser cutting.
Reading the Beam Profile Like a Floor Plan
Most people glance at a laser spot and see a dot. But if you treat that two-dimensional intensity map like an architect's floor plan, the picture changes completely. The brightest region becomes the main living area, the mid-level intensities are hallways, and the sharp drop-offs are exterior walls. Every bump or tilt in those boundaries tells you something about the optics upstream.
Instead of just measuring a diameter, you start reading the contour lines as if they were property lines. A lopsided peak is like a staircase placed too close to the entrance—it hints at a misaligned mirror or a stressed mount. Flat shoulders in the profile often correspond to apertures clipping the beam, much like a load-bearing wall that shouldn't be there.
The practical trick is to stop asking 'how big is the beam?' and start asking 'which rooms are too crowded, and where did the walls move?' Once you make that shift, a beam profiler stops being a simple meter and becomes a diagnostic floor plan. Small asymmetries that were easy to ignore suddenly stand out as design flaws.
Why Open Frame Doesn't Mean Unshielded Risks
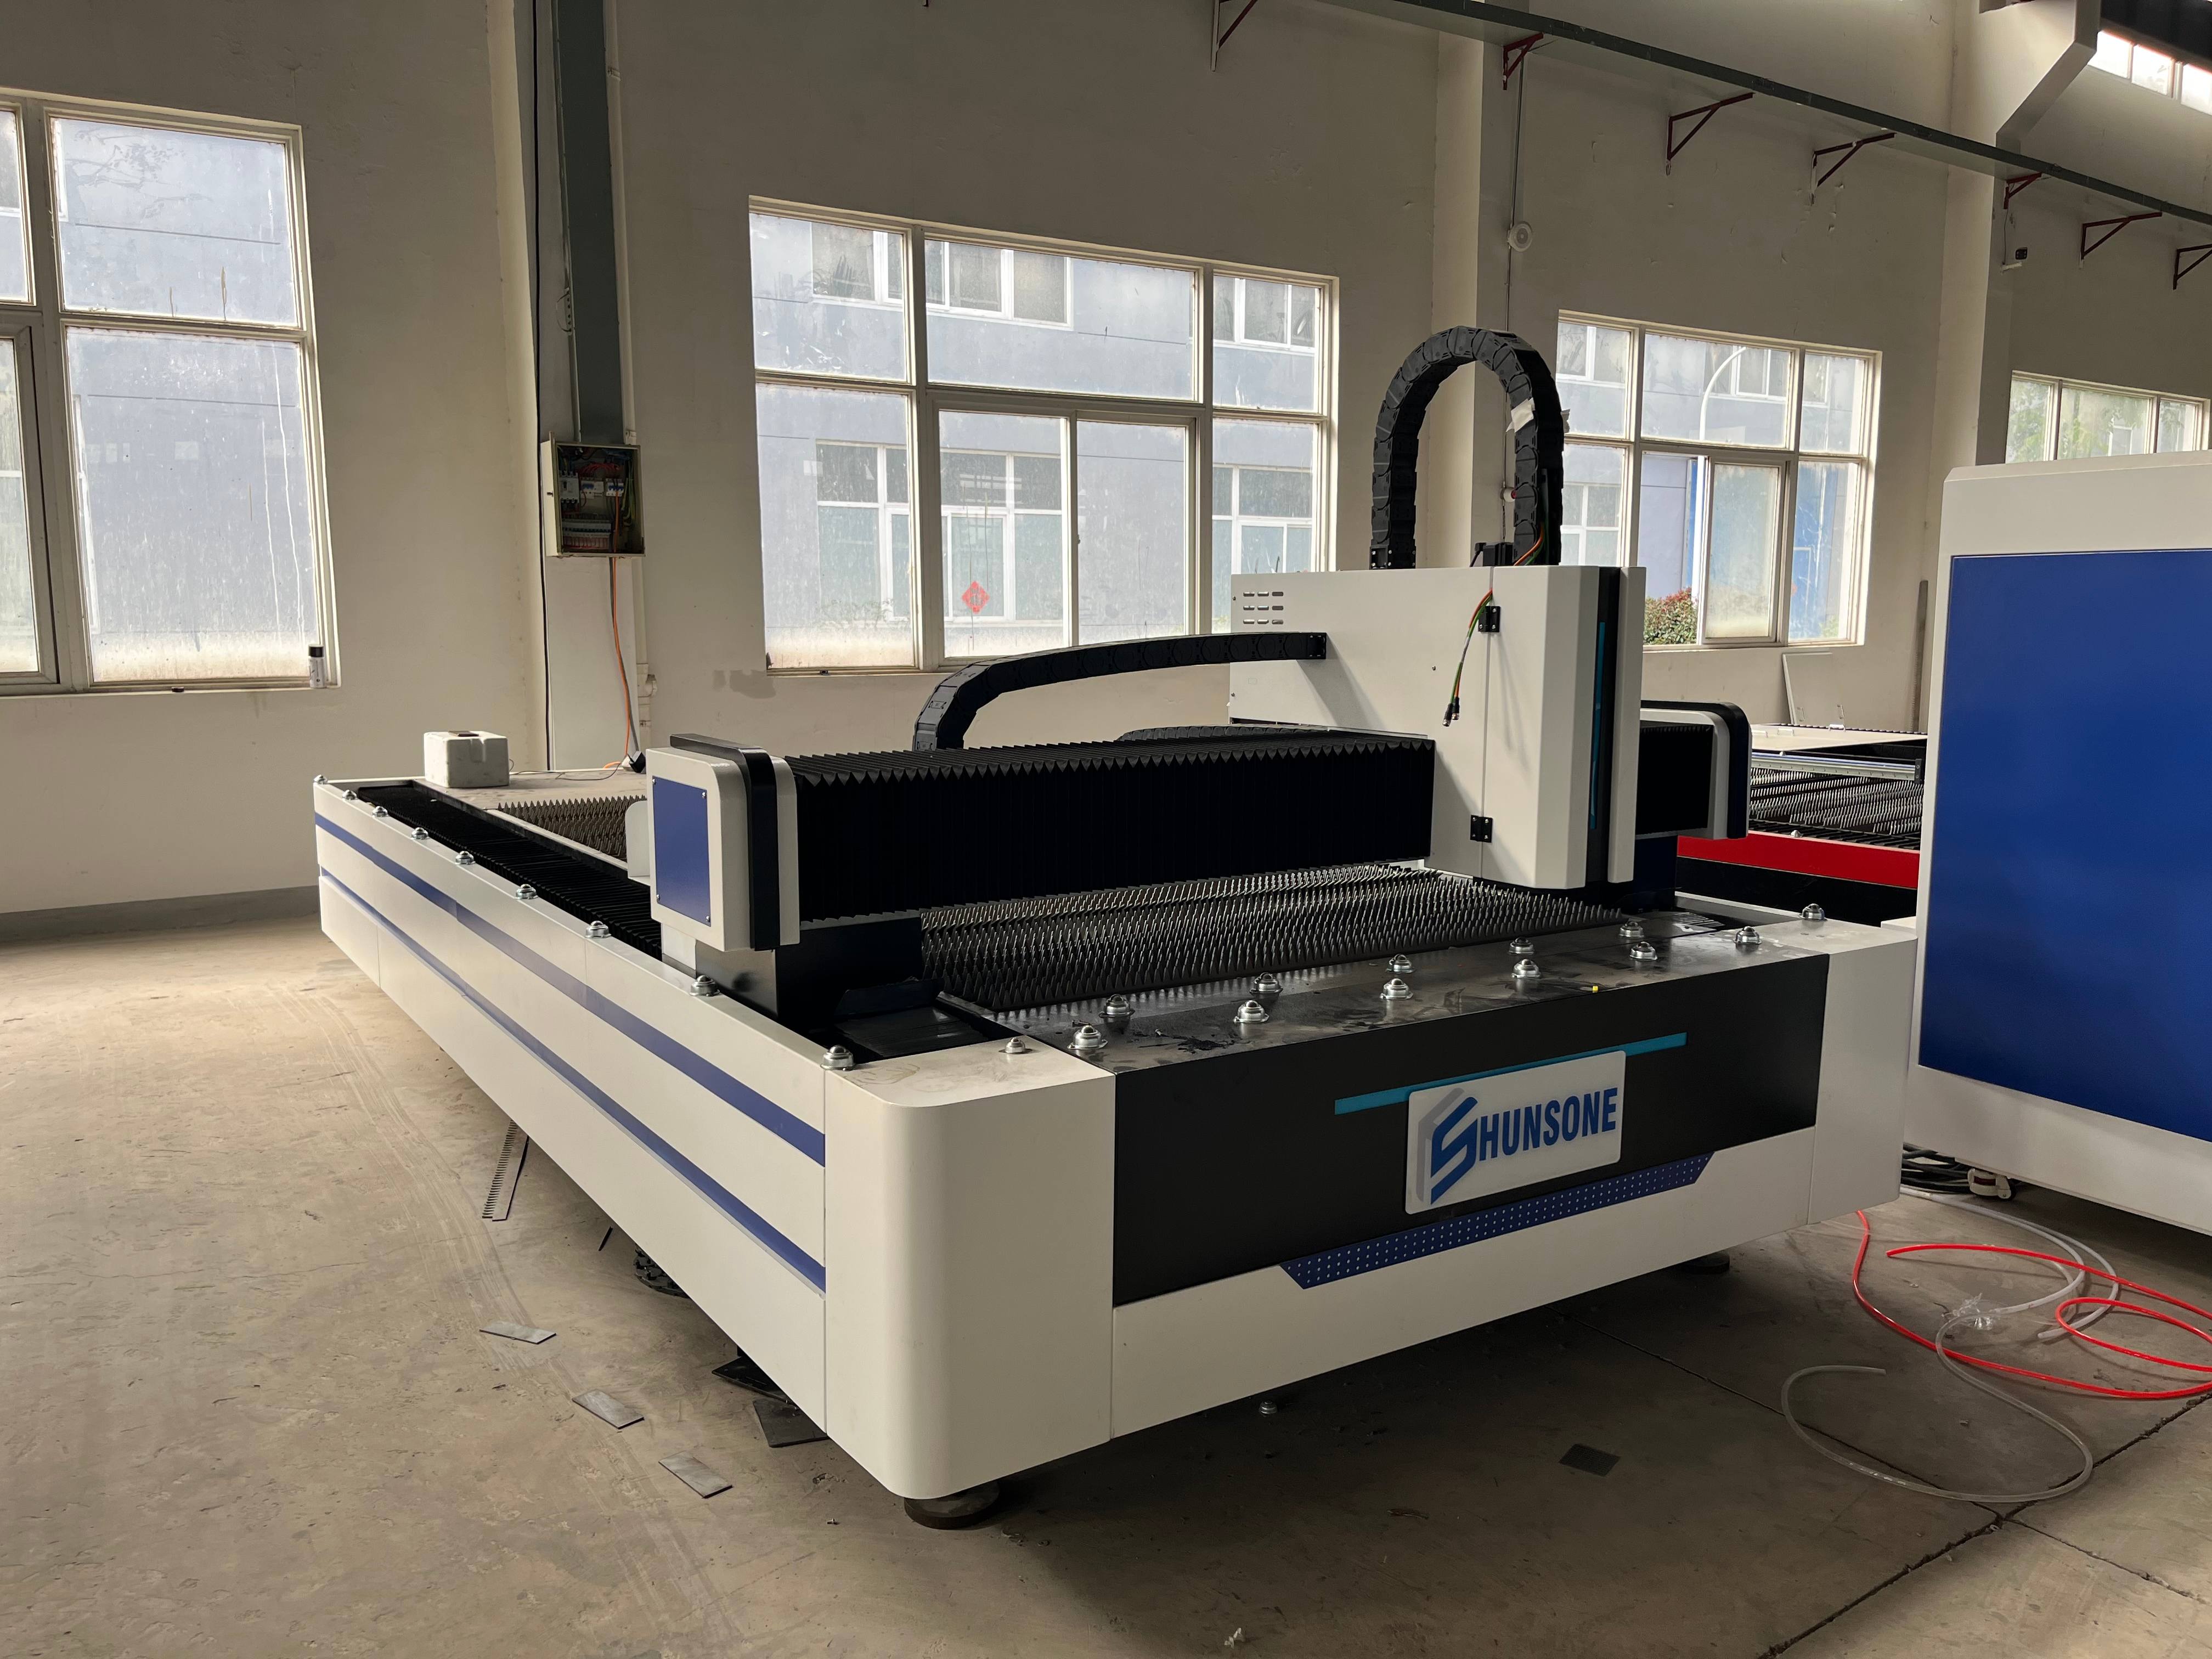
An open frame chassis can look like a liability at first glance—exposed boards, no sealed enclosure, air moving freely across every surface. But that visibility is not the same as vulnerability. The layout actually works in favor of reliability: heat dissipates before it builds up around sensitive ICs, and the lack of a tight shell means there is no trapped pocket for electromagnetic interference to rattle around in. Instead of relying on a metal box to do all the work, designers place shielding exactly where it matters—around clock generators, power stages, and high-speed traces.
That targeted approach often outperforms a fully enclosed design. A sealed chassis can create internal reflections that concentrate noise, while an open frame lets stray fields spread out and lose energy. Good grounding and short return paths handle the rest. This is why open frame power supplies and industrial boards still pass the same emissions and immunity tests as their boxed counterparts.
In short, the open frame is not a gap in protection but a different way of achieving it. The enclosure may be absent, but the design compensates with deliberate thermal flow, controlled impedance, and localized shielding. Risks are still managed—they are just managed closer to the source.
Matching Wattage to Metal Thickness Without Guesswork
Instead of relying on trial and error, start with a basic power-per-millimeter guideline. For carbon steel, a 1kW fiber laser can handle up to 6mm, but for stainless steel that same power struggles past 4mm due to reflective properties and thermal conductivity. Aluminum demands even more—roughly double the wattage per millimeter compared to mild steel. Write these ratios down; they’ll save you hours of ruined cuts.
Don’t forget that assist gas changes everything. Oxygen cutting allows lower wattage on thick mild steel because the oxidation reaction adds heat, while nitrogen cutting requires more power to blast through without burning edges. A quick way to estimate starting wattage: multiply material thickness in millimeters by 80–120 for steel, 150–200 for stainless, and 250–350 for aluminum. That gives you a ballpark, not a final setting.
Once you have that estimate, dial in by observing the cut edge. If you see heavy dross clinging to the bottom, you’re underpowered or moving too fast. If the edge looks melted or the kerf is too wide, back off the wattage. Keep a simple log of material type, thickness, gas, wattage, and speed. Over time, you’ll build your own cheat sheet that beats any generic chart.
The Real Cost of Cheap Assist Gas Filtration
On paper, a bargain filtration unit for assist gas looks like a smart way to trim capital expenses. The sticker price is lower, the installation seems straightforward, and the sales pitch often glosses over the finer points of media quality and housing integrity. But the real cost doesn’t show up on the purchase order. It appears weeks or months later, in the form of clogged nozzles, erratic cut quality, and unplanned downtime that eats away at whatever margin the cheaper system was supposed to protect.
Cheap filters tend to use lower-grade media that loads up quickly or, worse, sheds particles downstream. That forces operators to either replace cartridges far more often than expected or accept a gradual decline in cutting performance. The labor hours spent swapping elements, troubleshooting pressure drops, and reworking parts with dross or oxidation add up fast—often surpassing the initial savings within the first year. Meanwhile, premium filtration designs focus on consistent pressure retention and contaminant capture, which keeps the assist gas stream clean and the cutting table running without constant intervention.
There’s also the hidden toll on auxiliary equipment. Contaminated assist gas accelerates wear on solenoids, regulators, and even the laser head’s protective lens. A filter that lets fine particulates through doesn’t just produce a bad cut; it quietly shortens the life of expensive downstream components. When you factor in those repair and replacement cycles, the “cheap” option becomes a recurring operational liability rather than a one-time cost. Smart shops learn to evaluate filtration not by the invoice alone, but by the total cost of ownership across every shift it touches.
Calibration Routines That Keep Cut Edges Burr-Free
Dialing in your cutting equipment goes far beyond a quick glance at the blade. It starts with a systematic check of the clearance between the upper and lower cutting edges—often just a few thousandths of an inch—because even a slight mismatch lets material fold instead of separate, leaving behind those stubborn burrs. Paired with a consistent measurement of ram speed and hold-down pressure, you create a feedback loop where every adjustment is tied to what the edge actually tells you after each test cut.
A reliable routine includes running a short test strip at the beginning of every shift, and again after any tooling change or material batch switch. Feel the cut edge with a gloved thumb: a smooth, cool surface means the shear angle and penetration depth are still aligned. If you catch a rough or warm edge, back off the penetration slightly and re-check the blade gap before making another pass. This hands-on habit catches drift early, before burrs become a downstream cleanup problem.
For harder alloys or stacked sheets, consider a two-stage calibration: first set the blade gap on a known soft substrate, then fine-tune using the actual production material. Record your settings for each material thickness and temper—not as a fixed recipe, but as a living reference that gets updated when edge quality shifts. Over time, this turns calibration from a reactive fix into a preventive rhythm, keeping burr-free cuts the default rather than the exception.
When an Open Type Machine Outperforms an Enclosed One
Think of a workshop where the machine’s guts are fully visible—wires, belts, and mounting points exposed. That’s an open type setup. When you need to swap a worn bearing or reroute a cable in the middle of a job, the open frame lets you reach everything without dismantling half the unit. Enclosed machines look tidy, but their panels often hide exactly the parts you need to access quickly. For maintenance-heavy tasks or custom retrofits, the open design saves real time and frustration.
Open type machines also shine when heat is the enemy. Without a sealed cabinet trapping warm air, airflow moves directly across motors and controllers, keeping temperatures lower during long continuous runs. This matters in environments like print shops or small-batch manufacturing, where an enclosed unit might need extra cooling fans or even shut down to avoid thermal overload. A well-designed open frame can simply keep working.
Then there’s the matter of adaptability. If your process changes often—say you need to add a sensor, mount a different tool head, or lengthen a travel axis—an open machine gives you mounting holes and structural rails ready to accept new parts. An enclosed machine often forces you to cut through its casing or accept that the upgrade just won’t fit. For anyone who treats equipment as a starting point rather than a finished product, the open type is the practical choice.
FAQ
Look beyond the wattage. Pay attention to the gantry rigidity, the quality of the linear guides and rack-and-pinion system, and how well the frame absorbs vibration. A machine that shakes during rapid direction changes will never hold tight tolerances, no matter how powerful the laser source is.
It speeds up material handling noticeably. You can use an overhead crane or a forklift to drop a full sheet directly onto the table without fighting a bulky enclosure. Operators also find it easier to reach small cut parts from the sides, which cuts down on retrieval time between jobs.
A 1500W to 3000W source is usually the sweet spot. Below that, cutting 10mm steel becomes slow and edge quality suffers. Above that, you gain speed but also higher power consumption and more expensive replacement parts, so the extra capacity only pays off if you regularly cut thicker or highly reflective materials.
Burr formation often comes down to three things. The assist gas pressure must match the material thickness, the nozzle standoff distance has to stay consistent, and the cutting head height sensor needs to react fast enough over uneven sheet surfaces. Cheaper machines cut corners on the height sensor, which leads to inconsistent kerf width and burrs.
Yes, but only if the laser source has proper back-reflection protection and the control software limits power when the beam reflects. Copper and brass reflect a large portion of the laser energy, and without that protection the reflected beam can travel back into the fiber and destroy the pump diodes or the delivery cable.
Cleaning the protective window below the cutting head is the biggest one. Because the work area is open, dust and metal spatter settle on the lens faster than people expect. A dirty window absorbs laser energy, overheats, and eventually cracks, which then allows debris into the focusing lens and ruins the cutting head.
Plan for at least one meter of clear space on all sides, plus extra room for sheet loading equipment and part removal carts. The open design does not contain the laser beam fully, so you need a safety perimeter with light curtains or interlocked barriers to prevent anyone from walking into the beam path during operation.
Usually it is mechanical wear rather than laser degradation. Loose belts, worn pinion gears, or contaminated linear rails create backlash and positioning errors. Regular checks of the rack-and-pinion mesh and re-tensioning of the drive belts keep the motion system accurate, which directly preserves the cut precision.
Conclusion
Getting the most from an open type fiber laser cutter means reading the beam profile the way an architect reads a floor plan—small distortions in energy distribution show up later as kerf taper or dross. Open frames don't automatically mean greater danger, but they do demand a realistic look at light leakage, fume extraction, and where the operator stands during piercing. Matching wattage to metal thickness isn't a guessing game; it's a discipline where too little power forces slow feeds and too much power burns edges. The trick is knowing the machine's real sweet spot, not just the spec sheet.
Cheap assist gas filtration rarely stays cheap once contaminated lenses and unstable pressure eat into cut quality. Regular calibration routines—checking nozzle centering, focus position, and rail alignment—are what keep edges burr-free over months of daily use. And while enclosed machines make sense in some high-volume shops, an open type cutter often shines in long-sheet work, oversized parts, or tight layouts where quick access and simpler automation matter more than complete enclosure. Those practical trade-offs, not marketing checklists, decide whether an open frame is truly the better tool.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/