U-arm Open Flame RR Machine Factory How It Works and Why It Matters for Manufacturers
2026-09-23
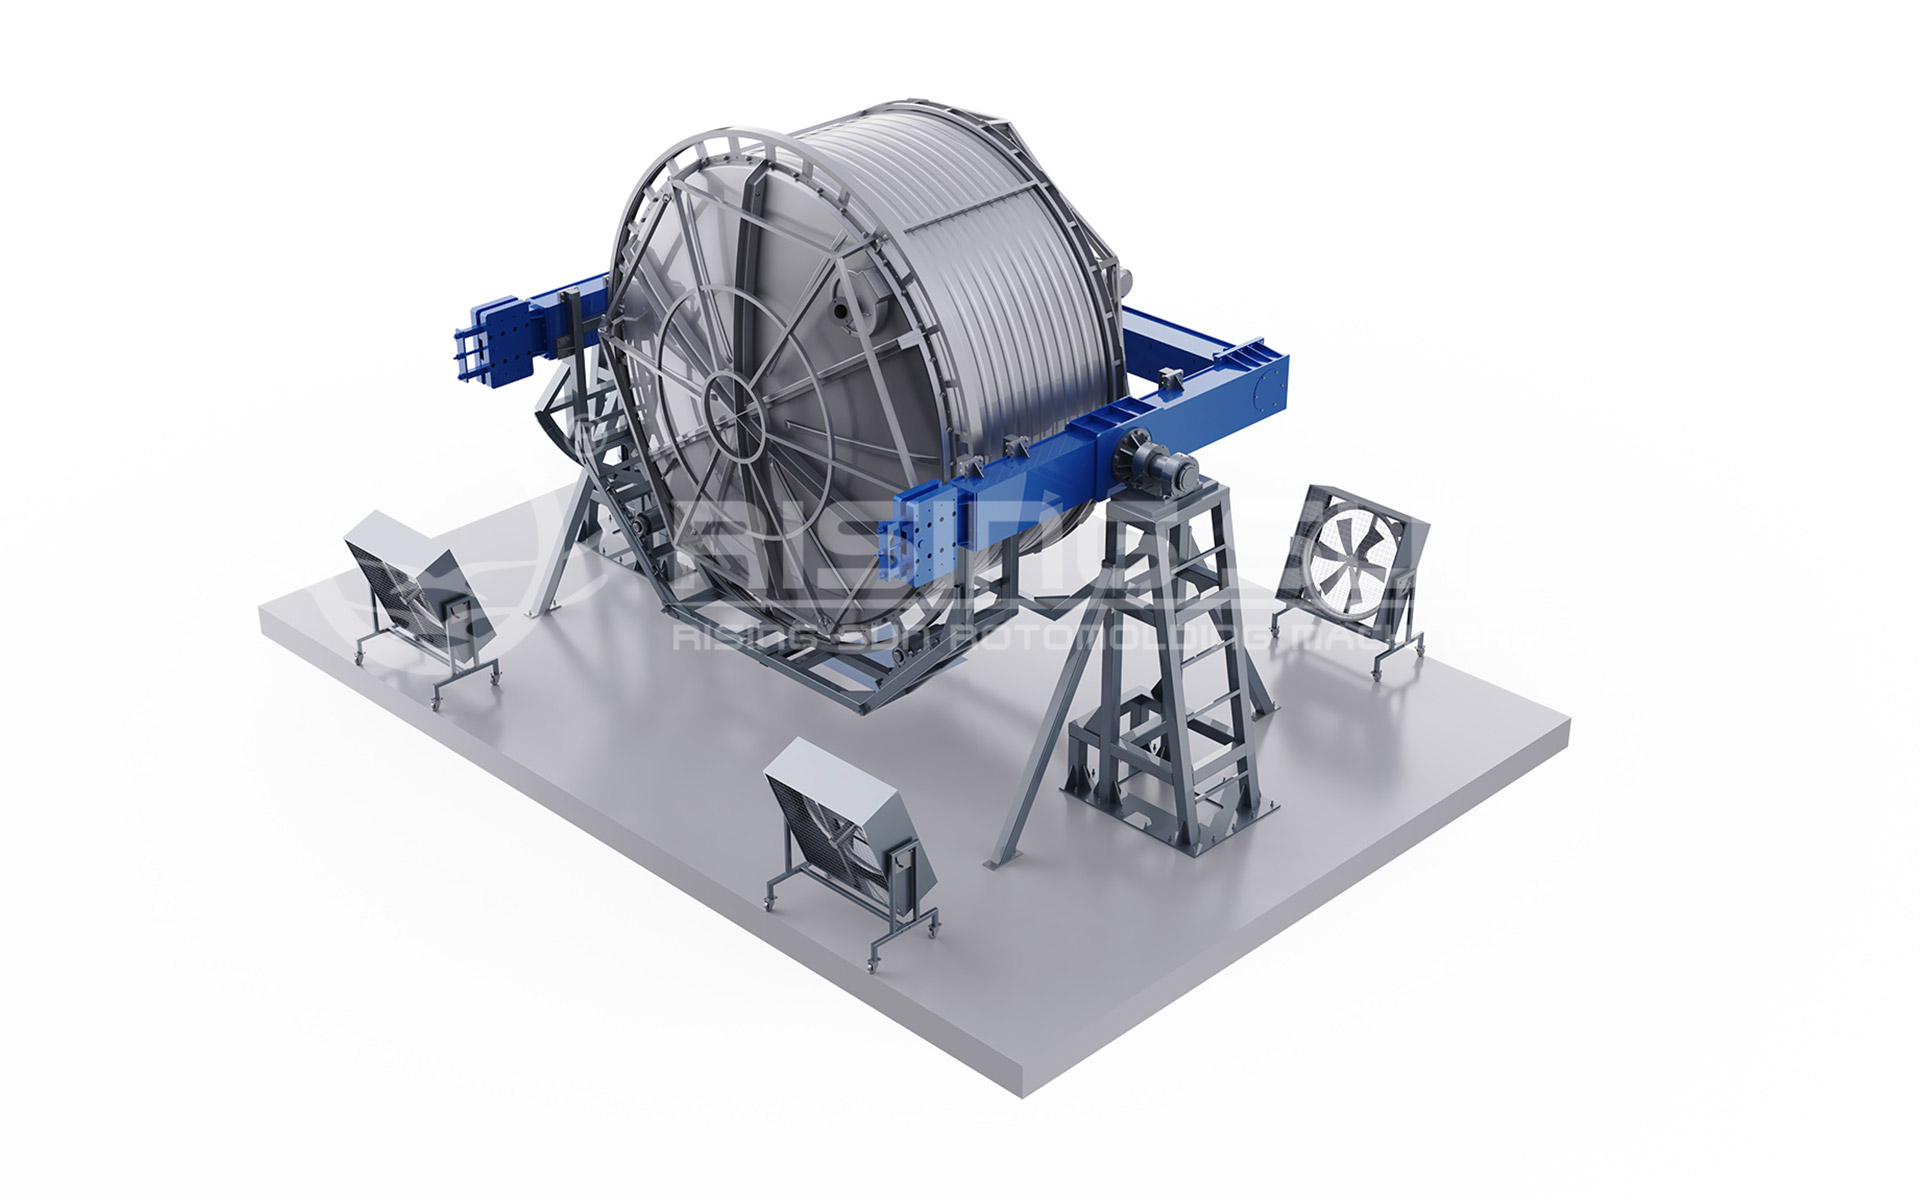
Rotational molding hasn’t stayed static, and neither have the machines behind it. The U-arm open flame RR machine is a prime example—purpose-built for uniform heating, easier mold access, and production runs that don’t compromise on consistency. Here’s a look at how it works in a Rising Sun factory, and why that design is starting to matter more for manufacturers balancing cost, output, and part quality.
Why the U-Arm Frame Is the Real Star of Open Flame RR Machines
Most people fixate on burner output or drum rotation speed when sizing up an open flame RR machine, but the U-arm frame quietly does the heavy lifting. That single piece of bent steel isn't just a mounting bracket—it dictates how evenly heat wraps around the drum, how stable the whole rig stays during long roasts, and whether your chaff collection actually works without shaking loose. You can bolt the finest infrared burner onto a flimsy rail system and still get scorched patches near the edges. The U-arm changes that by holding the drum at two precise points, letting the flame breathe across the full cylinder instead of concentrating in one hot stripe.
Another overlooked advantage is thermal flex tolerance. Open flame roasting cycles swing from ambient to over 400°F in minutes, and cheap frame designs warp enough to throw drum clearance out of whack by mid-session. A properly engineered U-arm absorbs that expansion without transferring stress to the drive shaft or front bearing. That means the gap between the flame nozzle and drum surface stays consistent from first crack to cool-down—so your roast curve actually matches what you logged last week, instead of drifting because the geometry shifted under heat.
Then there's the maintenance angle. Because the U-arm wraps around the rear of the drum rather than cluttering the front, you get direct access to the trier, sight glass, and drop door without unbolting half the frame. Swap a thermocouple, clean the exhaust elbow, or replace a worn drum paddle in minutes—not an afternoon. That open-sided design also lets you see the bean mass tumbling without craning your neck around a support strut. In a production roastery, those small ergonomic wins translate into faster turnaround between batches and fewer excuses to skip a deep clean.
The Flame Path and Roller Timing That Prevent Line Stoppages
On most continuous lines, the flame path is treated as a fixed setting, but it's the first thing I adjust when edge cracks start appearing. The burners along the width don't just supply heat; they shape the viscosity profile across the ribbon. If the outer flames overlap too early, the edges get hotter than the center, and the differential expansion shows up as a wave that travels downstream. A better setup staggers the flame tips so each burner's hot zone tapers into the next, keeping the cross-width temperature within a 5°C band. That band is what lets the glass pass through the forming rollers without buckling.
Roller timing is rarely about absolute speed. The issue is phase alignment between adjacent rolls, especially where the ribbon has cooled enough to become elastic. A roll running half a tooth out of phase creates a repeating slip-stick cycle that builds tension at the edge guides. Once that tension exceeds the edge strength, you get a snap and a full stop. We solve it by setting the drive offsets so that each roller's surface speed lags the previous one by 0.2–0.4%, not by matching them exactly. That intentional slippage dampens the harmonic instead of amplifying it.
The two systems have to talk to each other. If the flame path shifts because of a burner cleaning cycle, the viscosity changes slightly, and the roller timing that worked an hour ago now feeds a wave into the next section. A simple fix is to tie the roller speed offsets to a pyrometer reading near the last forming roll, not to the line master speed. When the edge temperature dips, the control loop advances the adjacent roller phase by a fraction of a degree. That small correction keeps the ribbon from ever reaching the critical stress point where a stoppage becomes inevitable.
Heat Management Without Warping on Thin and Thick Stock
Thin stock warps fast because it can't absorb much heat, so you have to feed it in short bursts and let the metal cool between passes. A copper or aluminum backing bar behind the weld pulls heat out quickly and keeps the panel flat. Skip around instead of running one continuous bead; weld an inch here, move to the opposite side, and come back after the glow fades.
Thick sections fail differently: they soak up heat and then release it unevenly as they cool, pulling the joint out of alignment. Preheat the area to around 200–300°F before welding to reduce the temperature gap, and use a slower travel speed so the heat spreads instead of pooling. Clamp the work to a heavy table or jig, but leave a little room for expansion rather than locking it rigid. After welding, let it cool in still air or under a welding blanket; quenching thick stock is asking for a banana-shaped part.
Open Flame RR Against Enclosed Chambers What Experienced Operators Prefer
Most operators who have run both an open flame reverse flow cooker and an enclosed chamber for any length of time will tell you the reverse flow offers a level of direct heat control you just don't get inside a sealed cabinet. With the fire burning right under the cook chamber and smoke forced through a baffle plate before rolling back over the meat, you can tweak airflow, add a split of hickory, or shift the protein to a hotter zone without opening a door and losing all your heat. That kind of minute-by-minute fire management does more than keep temperatures steady—it builds bark that snaps and fat that renders clean instead of going soft.
Enclosed chambers, on the other hand, are built for consistency. They hold moisture, run on less fuel, and hold a set temperature for hours with almost no attention. But that same sealed environment is exactly why a lot of experienced cooks shy away from them when the end result matters. The air inside an enclosed chamber tends to get humid and still, which can steam the outside of a brisket or pork shoulder rather than letting it dry and form a proper crust. You can still make good food in one, but you're fighting the design if you want the kind of texture and smoke penetration that open flame reverse flow produces naturally.
That's not to say an enclosed chamber is useless—far from it. Plenty of operators keep one around for overnight holds, sausage, or holding finished meats while the open flame rig handles the main cuts. But when asked what they actually prefer for a competition cook or a big weekend service, long-time operators tend to point at the open flame reverse flow. The reason is simple: you can always dial back a live fire and let it cruise, but you can't add real fire character to a sealed box after the fact.
The Daily Walk-Around Checks That Catch U-Arm RR Issues Early
Before the shift even starts, a slow walk around the U-arm reveals more than any dashboard ever could. You learn to notice the slight angle change where the arm meets the pivot, the way a fresh grease smear spreads unevenly after last night's run. A quick hand on the roller housing tells you if heat is building where it shouldn't, and that's often the first whisper of a bearing starting to bind. Nobody taught this in a manual, but after a few hunches pay off, you trust the feel of a surface more than a vibration readout.
The key is building a mental baseline for what normal looks like on your machine, then catching the deviations that others dismiss. Loose fasteners near the RR block don't always rattle loudly, sometimes they just leave a faint rust dust line that wasn't there Tuesday. While checking those points, you might spot a hairline crack forming at a weld joint where paint flakes in a pattern that repeats every few inches. Catching it at this stage means a twenty-minute touch-up instead of a mid-shift failure that puts the whole line down while maintenance hunts for a spare arm.
Most crews rush through the walk-around as a formality, but the operators who rarely see surprise downtime treat it as a conversation with the equipment. They run a finger along the RR contact surface, listening for the faint irregularity that suggests a flat spot developing on the roller. They compare today's bolt head positions with yesterday's marker scratches. It takes five extra minutes, but those minutes buy back hours of unplanned repair and keep the U-arm tracking true through the long afternoon pull.
Figuring Payback on a U-Arm Open Flame RR Machine for Your Plant
When you're weighing whether that U-arm open flame RR machine makes sense, the first step is nailing down real numbers. The sticker price is just the beginning—factor in freight, rigging, electrical and gas line upgrades, and any downtime during installation. You also need a solid baseline of what your current process actually costs per part, including fuel, labor, rework, and scrap. Without that baseline, any payback figure is just a guess.
A practical way to approach it is to calculate your net annual savings—subtract the new machine's estimated operating costs from your current total annual costs, then divide the fully installed machine price by that number. If you land around two to three years, it's usually a comfortable fit for most plants. But don't stop there. Run the numbers again assuming 15% lower throughput or an extra week of unplanned downtime. If the payback stretches past four years under those conditions, you may want to negotiate harder on price or look at a different burner configuration.
One thing that often gets skipped is the value of consistency. An open flame RR machine with a U-arm design can tighten your temperature profile enough to cut rejects noticeably, and that improvement doesn't always show up in a simple fuel-cost comparison. Also check what your local air permit will require—adding a new combustion unit might trigger stack testing or emissions monitoring that eats into first-year savings. Finally, ask the vendor for a realistic resale or trade-in value after five years. That residual can shave several months off your calculated payback and often tips the decision when two machines are otherwise close.
FAQ
It applies a direct, controlled open flame to metal surfaces or workpieces passing along a linear or rotary path. The U-arm frame holds the burner assembly steady, which lets operators treat long sections, rings, or irregular shapes without constantly repositioning the part.
The U-shaped arm cradles the workpiece from two sides or top and bottom, so the flame reaches multiple faces at once. That geometry cuts down on hot and cold spots that come from single-point torching, making repeatability easier for production runs.
In most factory contexts, RR stands for ring or round rolling, though some shops use it for rotary or reciprocating motion. The key is that the machine supports round workpieces—such as rolled rings, cylinder ends, or circular blanks—while the open flame performs heating, stress relief, or surface conditioning.
Open flame gives faster access for loading and unloading, and it works well for parts that don't fit neatly inside a furnace chamber. It also allows partial heating—say, only a flange or weld zone—without soaking the whole component, which saves energy and cycle time.
Look for flame monitoring with automatic shutoff, guarded gas lines, sturdy U-arm locking mechanisms, and clear ventilation requirements. Operators need training on flashback prevention and proper startup/shutdown sequences because the flame is exposed, not behind a sealed door.
By eliminating the need to move parts in and out of a large furnace, the U-arm Open Flame RR Machine shortens heat-up and cool-down cycles. Shops often see a jump in daily output for ring rolling, weld preheating, or local stress relief tasks, especially when the part flow is continuous.
Yes. Many versions support PLC controls, conveyor or roller feeds, and robotic part handling. The U-arm's fixed geometry actually helps automation because the flame position stays predictable, so a robot can place parts without constant recalibration.
Confirm the machine's heat output matches your material thickness and alloy type, check the gas supply requirements, and make sure the U-arm opening can accommodate your largest part diameter. Also think about floor space and exhaust routing, since open flames need adequate air exchange.
Conclusion
The U-arm open flame RR machine earns its place on the plant floor because the frame itself does more than hold burners. That U-shaped structure keeps the flame path steady while the rollers stay timed to the strip speed, so a minor tension change doesn't turn into a jam or a line stoppage. On thin stock, the open flame can be backed off and the roller gap adjusted without robbing heat from thicker sections, which is why operators rarely see edge wave or center buckle even when running mixed gauges back to back.
When you set an open flame RR unit beside an enclosed chamber, the real difference is access and control. Experienced crews tend to prefer the open design because they can watch flame impingement and tweak burner angles mid-run, while enclosed chambers hide the exact point where heat concentrates. Daily walk-arounds should center on U-arm alignment, roller wear, and flame nozzle cleanliness; spotting a clogged port or a drifting arm early prevents a full rebuild later. Payback usually arrives sooner than expected once you count fewer rejected coils, less downtime from thermal warping, and the ability to run both light and heavy stock without swapping major components.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com